


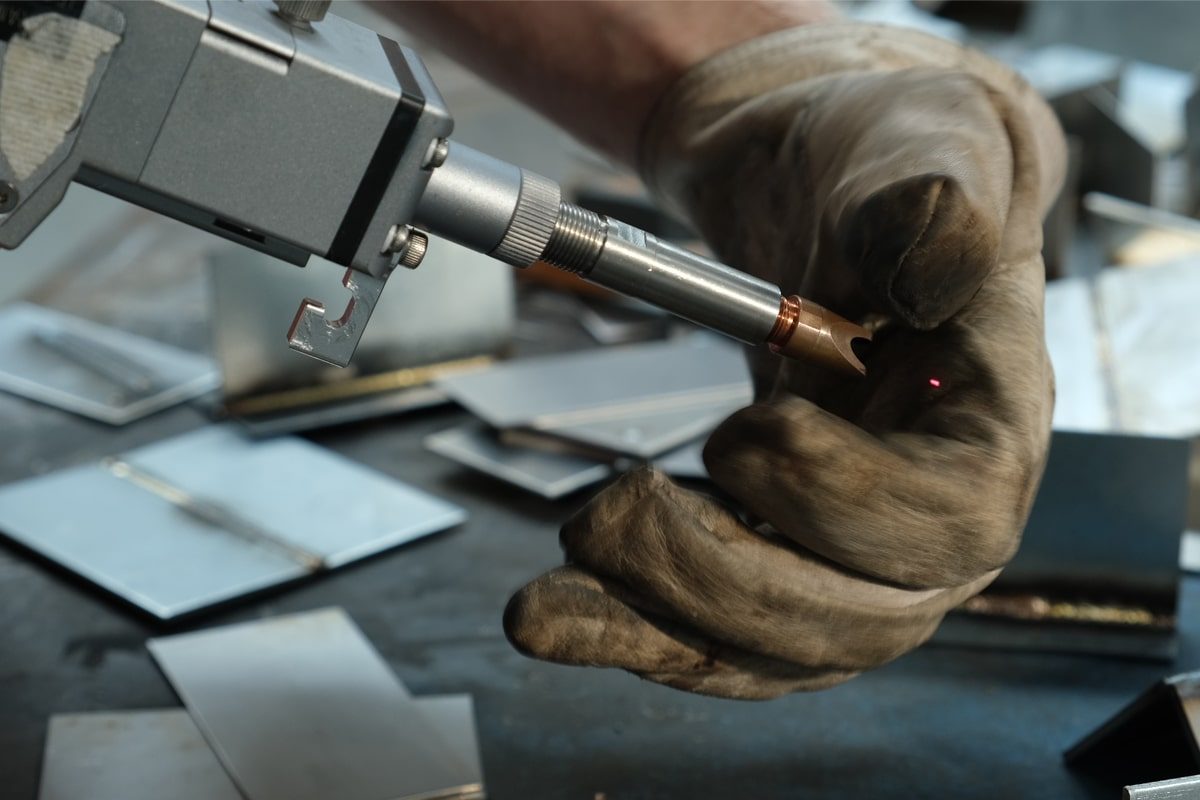
Laser Welding Machines: Comprehensive Guide
Laser welding has emerged as one of the most significant innovations in metal joining technology over the past two decades, fundamentally changing the economics and quality landscape of precision fabrication. Where traditional arc welding processes such as TIG and MIG have dominated for decades, fiber laser generators now enable joining speeds, penetration precision, and heat-affected zone control that conventional processes cannot approach. Yet laser welding machines represent a substantial capital investment, require different operational considerations than arc welding, and present a distinct set of technical requirements and safety considerations that fabrication shops must understand before making the technology transition.
This comprehensive guide is designed for manufacturing engineers, fabrication shop managers, and equipment buyers evaluating laser welding technology for the first time, or seeking to deepen their understanding of how fiber laser welding machines work, what materials they can join, what they cost to operate, what hazards they present, and how to maintain them for reliable long-term performance. The guide covers the fundamental technology, the genuine advantages that make laser welding compelling for specific applications, the real limitations and drawbacks that should inform the technology decision, the installed and operating costs, the range of metals that can be welded, the applications where laser welding has achieved dominance or strong presence, the safety considerations specific to laser technology, and the maintenance and operation best practices that sustain laser welding equipment reliability.
The objective is to provide practical, factual information that enables informed decision-making — neither overselling laser welding as a universal solution nor dismissing it as a specialized niche technology. Laser welding machines are neither; rather, they are highly capable equipment optimized for specific application profiles that represent the majority of industrial joining in many sectors. Understanding what laser welding can do, what it cannot do, what it costs, and how to operate and maintain it safely forms the foundation for technology decisions that will benefit fabrication facilities for years to come.
Table of Contents
Advantages of Laser Welding
Laser welding machines offer genuine technical and economic advantages over arc welding processes in applications where those advantages align with the production requirements. This section examines each major advantage in detail.
Precision and Accuracy
The focused beam from a fiber laser generator achieves spot diameters at the workpiece of 0.2 to 0.8mm, depending on the optical configuration, producing welds with widths that are similarly narrow. This precision enables joining in locations and on part features that arc processes cannot access without risk of thermal damage to adjacent components. The weld cross-section is highly repeatable from part to part when running a programmed laser welding machine, producing dimensional consistency that is difficult to achieve with manual TIG welding.
The heat-affected zone adjacent to the laser weld is minimized due to the concentrated energy input and high travel speed, meaning that base material properties are better preserved in the area surrounding the weld. This is particularly important for materials and applications where heat-affected zone properties directly affect service performance. In medical device and aerospace applications, this precision is literally a competitive necessity — alternative arc welding processes produce wider HAZ and greater weld variability that fails to meet the stringent quality requirements of regulated industries. Laser welding is the preferred process for these applications specifically because of the precision and consistency it delivers.
Speed and Efficiency
Laser welding travels along a joint at speeds five to forty times higher than manual TIG welding on comparable materials and thicknesses. On 2mm stainless steel — a benchmark material in medical device and food equipment fabrication — laser welding achieves 8 to 15 meters per minute compared to TIG’s 0.3 to 0.8 meters per minute. This speed advantage directly multiplies productive output per welding station and per hour. For a facility producing automotive body panels, medical device housings, or electronic enclosures at high volume, the speed difference between laser welding and TIG welding is the single most commercially significant factor determining production capacity and labor cost per unit.
Energy efficiency is also superior in laser welding: the fiber laser generator’s electrical-to-optical conversion efficiency of 30 to 45 percent means that a substantial fraction of electrical input becomes useful laser output, rather than being dissipated as waste heat as in many arc processes. This efficiency translates to lower operating energy cost per meter of weld produced, contributing to the overall cost-of-ownership advantage of laser welding in high-volume production environments.
Minimal Heat-Affected Zone
The narrow heat-affected zone of laser welding — often less than 1 to 2mm on each side of the weld centerline, compared to 3 to 10mm or more in arc welding — has profound implications for distortion, mechanical properties, and post-weld processing. Parts welded by laser welding exhibit less thermal distortion, require less or no post-weld straightening, and maintain more consistent mechanical properties across the entire cross-section than arc-welded parts.
For thin-sheet metal applications, this HAZ advantage is particularly valuable. A stainless steel panel welded by TIG welding may require 10 to 30 minutes of straightening and flattening after welding to restore flatness for assembly. The same panel welded by laser welding emerges from the welding station flat and ready for the next manufacturing step. This single difference — eliminating post-weld straightening labor — often represents a cost saving of $1 to $5 per part across high-volume production. On materials used in aerospace and medical devices, where sensitization (precipitation of chromium carbides in stainless steel) can degrade corrosion resistance in the heat-affected zone, laser welding’s narrow HAZ is a technical necessity rather than a convenience.
Versatility and Automation Integration
Laser welding machines integrate readily with robotic arms, CNC gantries, and automated production cells. The non-contact process — with the welding head maintaining a standoff distance of several centimeters from the workpiece — allows the head to follow complex three-dimensional weld paths without the contact force considerations that mechanical processes impose. Automated laser welding cells routinely achieve laser-on-time fractions above 80 percent, capturing the speed advantage of the laser generator across extended unattended operation.
This automation capability is fundamentally different from arc welding automation. A TIG welding robot exists and is used in industry. Still, its programming complexity and the process’s sensitivity to joint fit-up and thermal effects mean that automated TIG welding is most practical for fixed, high-volume jobs on consistent joint geometries. Laser welding automation is more flexible and can address a broader range of joint geometries and workpiece variations. For facilities running multi-shift production with overnight unattended operation, laser welding automation enables labor-free production during night shifts, multiplying the available production capacity without proportional increases in labor cost.
Non-Contact Process
Because the laser generator beam reaches the weld location without any physical contact between the welding head and the workpiece, the head does not wear from mechanical interaction and can be positioned precisely without the force-related wear that mechanical processes incur. This is particularly valuable for delicate assemblies where any mechanical contact force could distort the part.
Laser welding machines deliver genuine technical advantages across precision, speed, heat management, automation compatibility, and process cleanliness. These advantages are most impactful in applications involving thin to medium gauge materials, high production volumes, and parts where dimensional consistency and minimal distortion are quality requirements. For facilities that match these profiles, laser welding is not a luxury option but rather a technology that becomes increasingly necessary as production demands escalate and quality requirements tighten.
Disadvantages of Laser Welding
Laser welding technology has genuine limitations and drawbacks that are important to understand as part of a complete technology assessment. These disadvantages do not make laser welding unsuitable for its optimal applications, but they do define the contexts where other processes are more appropriate.
Initial Investment Cost
The capital cost of a laser welding machine — ranging from $20,000 for a basic handheld fiber laser welding machine to $80,000 or more for a fully integrated robotic cell — is substantially higher than the cost of comparable arc welding equipment. This upfront investment creates a threshold barrier for lower-volume fabrication operations and requires careful economic justification based on production volume and cost savings potential. A complete TIG welding station with power source, water cooling, and work station can be fully equipped for $5,000 to $15,000, placing laser welding at a three-to-five-times higher capital cost. This capital differential is real and is the primary reason why many job shops and low-volume fabricators continue to rely on arc welding despite laser welding’s speed and quality advantages.
Skill Requirements and Training Time
While laser welding requires less prior welding experience than manual TIG welding, setting up the process, programming the motion control system, and troubleshooting parameter problems require more technical knowledge than simply operating a laser welding machine on a pre-programmed job. The process has a steeper learning curve for setup and programming, though the operating skill requirement is lower.
An operator with no prior welding experience can learn to run a pre-programmed laser welding cycle and produce consistent results within 4 to 8 hours of training. This is dramatically faster than the months or years required to develop TIG welding competence. However, when problems arise — when a new material or thickness is introduced, and existing parameters do not work, or when joint geometry differs from previous jobs — the troubleshooting and parameter optimization require more technical knowledge than arc welding. A TIG welder can often sense a problem through feel and sound and adjust intuitively. A laser welding machine operator needs to understand the interaction between laser power, travel speed, focus position, and assist gas pressure, and needs to be able to modify parameters methodically to optimize performance. This technical knowledge requirement is the downside of laser welding’s lower operating skill threshold.
Limited Thickness Range
Mid-power fiber laser generators (1500W to 3000W) can penetrate 3 to 10mm of stainless steel, carbon steel, or aluminum, but struggle with thicker materials. Applications requiring single-pass welding of materials above 10 to 15mm typically require laser generators at 6000W or higher, or require multi-pass laser welding procedures that reduce the speed advantage compared to single-pass arc welding.
Reflective Materials
Highly reflective metals — particularly copper and brass — present challenges for fiber laser generators at 1064nm, as a significant fraction of the beam is reflected rather than absorbed. Special high-power laser generator configurations with protective optics, green-wavelength laser generators, or multiple laser generator systems are required for these materials.
Safety and Hazard Profile
Laser welding presents radiation hazards that are not present in arc welding, along with the conventional welding hazards of heat, fumes, and fire risk. Proper machine enclosure, operator training, and control of reflective surfaces are essential for safe operation.
Laser welding’s disadvantages include higher capital cost, a steeper setup and programming learning curve, limited penetration depth on very thick materials, difficulties with reflective metals, and specific safety hazards related to laser radiation. These limitations do not make laser welding unsuitable for applications where throughput, precision, and minimal distortion are primary objectives, but they do define the contexts where the technology is or is not economically rational.
Laser Welding Machine Costs
Understanding the cost structure of laser welding — both capital and operating costs — is essential for evaluating the economic case for the technology.
Capital Equipment Cost
A fiber laser welding machine system typically comprises several major cost elements: the fiber laser generator and power supply, ranging from $8,000 to $25,000 depending on power level (1500W to 6000W); the welding head and beam delivery optical system, typically $5,000 to $15,000; the motion control system (CNC gantry, robot arm, or manual positioning system), ranging from $3,000 for manual systems to $30,000 or more for robotic integration; and the chiller and supporting infrastructure. Total system cost typically ranges from $20,000 for a basic handheld system to $80,000 or more for fully automated robotic configurations.
The handheld laser welding machine at $20,000 to $30,000 is the entry point for many shops — providing flexibility and manual control for varied job types. A CNC gantry-mounted system for high-volume production of consistent parts adds $10,000 to $20,000 to the system cost. A fully integrated robotic laser welding cell with a six-axis robot, material handling, vision systems, and integrated process control can reach $80,000 to $150,000 or more for a turnkey installation. The capital tier selected must match both the production volume and the consistency and complexity of the parts being welded.
Operating Costs
Energy cost for a 2000W laser welding machine system during active welding is approximately 7 to 10 kW of total system power draw, resulting in energy costs of approximately $0.70 to $1.20 per hour at industrial electricity rates of $0.10 to $0.12 per kWh. Shielding gas cost is typically $0.50 to $1.50 per hour depending on gas type and local pricing. Wire consumables (where used) add additional cost depending on volume and material. Total operating cost per productive welding hour is typically $2.00 to $4.00 for consumables, energy, and gas combined, compared to $3.00 to $6.00 or more for arc welding processes when skilled operator labor costs are excluded.
Beyond these direct consumable costs, laser welding machines require periodic maintenance including optical component cleaning and replacement, laser tube replacement after 8,000 to 10,000 hours of operation (a cost of $5,000 to $15,000 depending on power level), and chiller maintenance. These periodic costs are lower than the continuous skilled labor cost of arc welding but should be factored into the total cost model when evaluating long-term operating economics.
Payback Analysis
For fabrication facilities operating laser welding machines at high enough utilization to keep the equipment busy across multiple shifts, the payback period on the capital investment is typically 18 to 36 months when labor cost savings from skilled welder wage differentials and post-weld finishing labor elimination are included in the economic model. A facility with a $50,000 laser welding machine investment, generating $25,000 to $40,000 in annual labor and finishing cost savings through elimination of skilled welder wages and post-weld finishing labor, will recover the capital investment within 18 to 30 months. After payback, the machine generates pure profit contribution as long as it remains in productive use — often 10 to 15 years of economic life for modern fiber laser equipment.
Laser welding machine capital costs are higher than arc welding equipment, but operating costs per productive unit of output are lower due to the speed advantage and elimination of post-weld finishing labor in many applications. The economic case for laser welding is compelling when production volume is high enough to fully utilize the equipment’s throughput capacity.
Welding Gas Requirements
Laser welding requires shielding gas to protect the weld pool and control cutting and oxidation, with specific gas selections depending on the material being welded and the desired weld characteristics.
Gas Selection by Material
For carbon steel welding, compressed air or oxygen is often used as the shielding gas, with oxygen sometimes mixed with nitrogen at specific ratios. For stainless steel welding, argon is the standard shielding gas, chosen for its inertness and the oxide-free surfaces it produces. For aluminum welding, argon is also the standard, though helium is sometimes added to increase heat input on thicker sections. For reactive metals such as titanium, pure argon with trailing gas backup is required to prevent oxidation of the weld pool and heat-affected zone.
Gas Purity and Flow Rate
The purity of shielding gas has a direct impact on weld quality — gas containing water vapor or other contaminants will produce inferior weld surfaces and subsurface porosity. Industrial-grade shielding gas with moisture content below 20 ppm (parts per million) is standard for precision applications. Flow rates typically range from 15 to 30 liters per minute depending on part geometry, workpiece size, and laser generator power.
Cost and Supply Considerations
Shielding gas can be supplied from bulk cylinders replaced by the supplier, from liquid nitrogen generators for on-site gas production, or from compressed air sources for applications where compressed air is acceptable. Bulk cylinder supply is typically most economical for continuous high-volume operations, while liquid gas generation is appropriate for very high-volume facilities.
Laser welding gas requirements are material-specific and depend on weld quality objectives and protective requirements. Proper gas selection, purity verification, and appropriate flow rates are essential for achieving target weld quality and are standard considerations in laser welding machine setup and operation.
Metals Compatible with Laser Welding
Laser welding machines can join a broad range of engineering metals, though the specific requirements and challenges vary significantly by material type.
Carbon Steel
Carbon steel welds readily with fiber laser generators using oxygen or air as the shielding gas. Welding speeds on carbon steel are high — typically 15 to 30 meters per minute on thin sheet. Joint quality is excellent, with minimal distortion and excellent strength. Carbon steel is one of the most straightforward materials for laser welding.
The ease of welding carbon steel reflects the material’s ideal combination of properties for laser welding: moderate reflectivity allows efficient laser generator energy coupling, adequate thermal conductivity allows heat to spread through the material at speeds compatible with laser welding travel speeds, and the material’s response to rapid heating and cooling produces welds with predictable properties and minimal defects. Automotive, appliance, and general industrial fabrication shops find that their carbon steel work is the easiest and most economical work to transition to laser welding.
Stainless Steel
Austenitic stainless steels (300-series) are ideal laser welding materials. The laser generator’s heat and narrow HAZ are particularly valuable for stainless steel because they minimize sensitization (chromium carbide precipitation) that can occur with wider heat-affected zones in arc welding. Stainless steel is a primary material for many laser welding applications in food equipment, medical devices, and architectural metalwork.
Sensitization in stainless steel occurs when the heat-affected zone reaches temperatures between 450°C and 900°C during arc welding, causing chromium to be depleted from the base material immediately adjacent to the weld and precipitate as chromium carbides. This depletion creates regions of reduced corrosion resistance that can lead to intergranular corrosion failure in certain environments. Laser welding’s narrow HAZ significantly reduces the volume of material that experiences this sensitization, making it the preferred process for stainless steel applications in food and beverage equipment, medical devices, and marine environments where corrosion resistance is critical.
Aluminum Alloys
Aluminum presents both advantages and challenges for laser welding. The high thermal conductivity of aluminum requires sufficient laser generator power to achieve penetration, and the reflectivity of aluminum at the 1064nm wavelength of fiber laser generators means that high-power laser generators or special beam modulation techniques are required for reliable welding. Once these challenges are addressed, aluminum welds very well at high speeds with excellent quality.
The reflectivity challenge is the most significant: aluminum reflects approximately 90 percent of incident 1064nm laser generator radiation when cold, and even when melting begins, the reflectivity decreases somewhat; it remains significantly higher than steel. This means that laser generators operating at 1064nm require special techniques or higher power levels to weld aluminum reliably. Some manufacturers use green-wavelength laser generators (515nm), which aluminum absorbs much more efficiently, though these are more expensive and less common than 1064nm fiber systems. Others use beam wobbling or pulsing techniques to initiate and maintain consistent welding. Aluminum welding by fiber laser is therefore more specialized than carbon steel or stainless steel welding, requiring specific equipment configuration and operator expertise.
Titanium
Titanium and titanium alloys can be laser welded effectively, particularly for aerospace applications where the combination of minimal distortion and high-quality welds is valued. Titanium requires inert gas shielding and sometimes special fiber laser generator configurations, but it is a well-established laser welding material. The reactive nature of titanium at elevated temperatures demands complete protection from atmospheric contamination during and after welding — requiring inert gas shielding at the weld point, trailing shields to protect the cooling weld pool, and sometimes backing gas to protect the underside of the joint. The reward for this care is exceptional weld quality: aerospace-grade titanium welding by laser produces welds with superior mechanical properties and microstructural consistency compared to arc welding, making laser welding the preferred process for critical aerospace applications.
Copper and Brass
Nickel Alloys
Nickel-based superalloys and corrosion-resistant nickel alloys are laser welded in aerospace applications where the combination of minimal distortion, minimal sensitization in the heat-affected zone, and high-quality welds makes laser welding preferable to arc welding.
Laser welding is compatible with a broad range of engineering metals including carbon steel, stainless steel, aluminum, titanium, and nickel alloys. Copper and brass present special challenges requiring higher-power or specialized laser generator wavelengths. Successful laser welding of any material requires appropriate laser generator power, shielding gas selection, and process parameter optimization. The ability to weld multiple material types on the same machine, through parameter changes rather than equipment changes, is one of the practical advantages of laser welding in job shops and contract manufacturers who encounter diverse material requirements.
Applications of Laser Welding
Laser welding has achieved significant presence in several major industrial sectors where its speed, precision, and low-distortion characteristics align well with production requirements.
Automotive Industry
The automotive industry is the largest market for laser welding machines globally, with applications including body panel joining, battery enclosure welding for electric vehicles, seat frame assembly, transmission housing welding, and precision component fabrication. The combination of high production volume, thin to medium gauge materials, tight dimensional tolerances, and the need for minimal distortion makes laser welding the dominant technology in these applications.
In automotive body panel manufacturing, fiber laser welding machines have become the standard technology at major OEMs and Tier 1 suppliers, replacing arc welding on high-volume production lines. The speed advantage — combining laser welding speeds with robotic positioning — enables production rates of 60 to 100 parts per hour per welding station, a throughput level that arc welding processes cannot approach. For battery enclosures in electric vehicles, laser welding is nearly the exclusive technology, chosen for its ability to produce hermetic seals with minimal heat input to the battery internals and consistent, repeatable weld geometry across thousands of units.
Electronics Manufacturing
Laser welding is widely used in electronics manufacturing for joining stainless steel and aluminum enclosures, joining precision components with minimal thermal distortion, welding hermetic seals on electronic packages, and joining dissimilar metals in electronic assemblies. The precision and minimal heat input that laser welding provides are particularly valuable in applications where thermal damage to sensitive electronic components must be prevented.
Medical Device Manufacturing
Medical device manufacturers extensively use laser welding for stainless steel enclosure welding, joining of surgical instruments, hermetic sealing of implantable devices, and precision component fabrication. The ability to produce clean, oxide-free welds on stainless steel with minimal post-weld finishing is particularly valuable in medical applications where surface cleanliness and weld appearance are quality requirements.
Surgical instruments — forceps, clamps, scissors with welded components — are manufactured almost exclusively using laser welding in modern production. The precision enables joining of delicate surgical geometries without distortion, the minimal HAZ preserves the temper and performance characteristics of stainless steel tool steel, and the clean weld surfaces meet the sterilization and biocompatibility requirements of medical devices. For implantable devices where hermetic sealing is a safety requirement, laser welding’s ability to produce consistent, defect-free welds is literally a regulatory requirement rather than a preference.
Aerospace and Defense
Aerospace applications of laser welding include precision titanium alloy welding on aircraft engine components, stainless steel welding in airframe structure, and dissimilar metal joining where the combination of minimal distortion and high-quality welds makes laser welding preferable to other processes. The aerospace industry values laser welding’s ability to minimize the heat-affected zone on reactive alloys and its compatibility with automated production cells.
Laser welding has become the dominant technology in high-volume production of thin to medium gauge materials in automotive, electronics, medical device, and aerospace applications. These industries represent the largest commercial markets for laser welding machines and the applications where laser welding’s speed, precision, and minimal-distortion characteristics provide the most compelling value.
Hazards Associated with Laser Welding
Laser welding machines present a specific set of hazards that are distinct from traditional arc welding and require appropriate control measures.
Laser Radiation Hazard
Fiber laser generators operating at 1064nm wavelength produce near-infrared radiation that is transmitted through the eye to focus on the retina. Direct or specularly reflected exposure to an unprotected eye can cause immediate and potentially permanent retinal damage. The injury mechanism is different from surface burns — the near-infrared energy passes through the eye’s surface and focuses on the retina deep in the eye, causing thermal damage at the focal point before any protective blink response can occur. In fully enclosed laser welding machines, the enclosure contains the beam during normal operation, reducing the effective hazard classification. During open-beam work, alignment, or maintenance, appropriate laser safety eyewear rated for the specific wavelength and optical density is essential. Reflective surfaces in the work area — polished metal fixtures, mirrors, or even jewelry — can redirect the beam unexpectedly, which is why reflective object control is an important safety practice in facilities doing open-beam laser work.
Heat and Fume Hazards
The focused laser generator beam generates intense local heat, creating fumes and particulate from vaporized material and heated surfaces. Adequate ventilation with fume extraction is essential, particularly when welding materials that generate hazardous fumes such as zinc-containing alloys (galvanized materials). Proper extraction equipment rated for the specific fume profile of the materials being welded is necessary.
Different materials produce different fume profiles requiring specific extraction approaches. Welding of galvanized (zinc-plated) steel produces zinc oxide fumes that can cause metal fume fever if inhaled — requiring local extraction right at the weld point. Stainless steel welding produces primarily iron and chromium oxides with minimal hazardous components if ventilation is adequate. Aluminum welding produces aluminum oxide particulate that is primarily nuisance dust but still requires local extraction to maintain air quality. Laser welding fumes are generally less voluminous than arc welding fumes due to the smaller heat input area, but local extraction is still essential for operator health and facility compliance with occupational air quality standards.
Electrical Hazard
Laser welding machines incorporate high-voltage electrical systems for the laser generator power supply and other components, delivering high currents to the laser generator assembly. Implementing appropriate electrical safety measures is critical; these include ensuring proper equipment grounding, enclosing electrical components within protective housings, and having trained personnel operate the electrical systems. Only qualified electrical technicians are permitted to work on power supply components or high-voltage circuits. Operators must not open the laser power supply housing or attempt electrical troubleshooting beyond simply verifying that the power is on and connections are secure.
Fire Hazard
Although less pronounced than in laser cutting applications, laser welding can generate sufficient localized heat to ignite combustible materials. Appropriate fire suppression equipment, workspace cleanliness, and awareness of fire risk are necessary precautions.
Mechanical Hazard
Moving parts in laser welding machines — robotic arms, CNC gantries, and motion control systems — present mechanical pinch and crush hazards. Appropriate machine guards, emergency stop systems, and operator training are essential.
Laser welding machines present specific hazards related to laser radiation, heat and fumes, electrical components, fire risk, and mechanical motion. Appropriate control measures, including machine enclosure, laser safety eyewear, ventilation, electrical safety, and mechanical guards, are essential for safe operation.
Filler Materials in Laser Welding
Laser welding can be performed with or without filler material, depending on the joint design and metallurgical requirements.
Autogenous Welding
Many laser welding applications are performed without filler material, relying on the base material to form the weld pool. This is appropriate for joint designs where the gap between parts is minimal, and the base material composition is satisfactory for the service requirement.
Wire-Feed Laser Welding
Some laser welding machines incorporate wire-feed mechanisms that introduce filler wire into the weld pool. This allows the operator to adjust the weld metal composition, bridge larger gaps between parts, and control weld bead height and width more precisely than autogenous welding.
Filler Material Selection
When filler wire is used, the material composition should match or exceed the base material properties. Stainless steel filler wire is used for stainless steel welding, mild steel wire for carbon steel, and aluminum welding wire for aluminum. The wire diameter and feed rate must be optimized to match the laser welding machine’s power level and travel speed.
Laser welding can be performed autogenously or with filler wire, depending on joint design and metallurgical requirements. Wire-feed laser welding provides additional process control and material composition options compared to autogenous welding.
Maintenance and Care of Laser Welding Machines
Regular maintenance and careful operational procedures are essential for sustaining laser welding machine reliability and performance over years of productive operation.
Regular Cleaning
The laser welding machine optical path, including mirrors and lenses, should be inspected regularly and cleaned of dust, welding spatter, and oxidized coatings that accumulate during operation. The frequency of cleaning depends on the specific materials being welded and the volume of welding — high-volume operations welding materials that generate significant particulate may require daily cleaning. Clean optics are essential for maintaining laser generator power output and weld quality.
For stainless steel welding, small amounts of particulate settle on optical surfaces. For aluminum welding, aluminum oxide dust can form a coating that absorbs laser generator energy and reduces effective power output. For materials like zinc-plated steel, zinc oxide particles can accumulate on optical surfaces. Each of these scenarios reduces the effective power delivery to the weld by 10 to 30 percent or more if allowed to accumulate. Regular cleaning — using optical-grade cleaning materials and avoiding touching optics with bare fingers — is a simple maintenance task that prevents most laser welding machine power loss incidents.
Alignment Checks
The optical path alignment should be verified periodically using a beam alignment test procedure. Misalignment can occur due to thermal cycling, vibration, or mechanical shock. Prompt realignment prevents performance degradation. Many laser welding machine operators perform this check weekly or monthly as routine maintenance. The alignment procedure typically involves marking the beam position on masking tape or marking paper at multiple points across the welding area and comparing the mark positions to the expected nozzle centerline — shifts in position indicate misalignment requiring correction. For operators unfamiliar with alignment procedures, the machine manufacturer’s service manual provides step-by-step guidance, or manufacturer technical support can walk through the procedure via phone or video conference.
Cooling System Maintenance
The laser generator cooling system requires regular attention. Water quality should be monitored, and distilled water should be used rather than tap water to prevent mineral accumulation. The chiller should be inspected regularly to confirm proper operation and adequate heat rejection. Temperature readings should be monitored to ensure the laser generator is not operating outside its specified thermal range.
Calibration and Parameter Verification
Laser welding machine parameters should be verified periodically to ensure they remain optimized for the current production workload. Output power should be measured using a laser power meter at regular intervals to verify that laser generator performance has not degraded below acceptable thresholds.
Routine Inspection
Regular visual inspection of the laser welding machine should cover the condition of optical components, signs of cooling system leakage, integrity of electrical connections, function of safety interlocks and emergency stops, and general machine cleanliness. Most manufacturers recommend monthly inspection as a standard maintenance practice.
Laser welding machine maintenance includes regular cleaning of optical components, alignment verification, cooling system care, parameter calibration, and routine inspection of safety systems and general machine condition. A structured maintenance schedule prevents the majority of performance degradation and extends the operational life of the equipment significantly.
Summary
This comprehensive guide has covered the full landscape of laser welding machine technology — from the fundamental advantages that make laser welding compelling for high-volume precision applications, through the real limitations that define when other processes are more appropriate, through the economic analysis that determines the financial case for laser welding investment, through the operational requirements including gas selection, material compatibility, and safety controls, to the maintenance practices that sustain reliable performance over years of productive operation.
The central message is that laser welding machines are highly capable equipment optimized for a specific set of applications that represent the majority of industrial joining in several major sectors. In applications involving high production volume, thin to medium gauge materials, tight dimensional tolerances, minimal distortion requirements, and materials where the minimal heat-affected zone of laser welding is particularly valuable, laser welding technology offers compelling advantages in speed, quality consistency, automation compatibility, and often in total cost of ownership.
Laser welding is not appropriate for low-volume custom work, for very thick materials beyond the penetration capability of available laser generators, for materials where extensive filler metal composition control is required for metallurgical reasons, or for applications where the capital investment cannot be justified against available production volume. In these contexts, traditional arc welding remains the appropriate process choice.
For fabrication facilities evaluating the technology transition, the decision framework should include thorough economic analysis encompassing capital cost, operating cost per productive unit, labor cost differentials, post-processing labor elimination, and the value of improved quality consistency and reduced distortion. When this analysis is performed rigorously, and the production volume is high enough to fully utilize the laser welding machine’s throughput capacity, the investment typically proves justified within an 18-36 month payback period.
The laser welding technology landscape continues to evolve — higher-power fiber laser generators are becoming more cost-effective, beam shaping technologies are improving performance on challenging materials like aluminum and copper, and integrated automation is making laser welding systems more accessible to mid-size fabricators. For new shops or shops planning technology transitions in the next 5 years, investigating laser welding capabilities for the core production workload is increasingly a matter of competitive necessity rather than optional optimization.
Get Laser Welding Solutions
Implementing laser welding technology requires selecting the right machine configuration and establishing operational procedures that ensure consistent high-quality performance from the first production run onward.
AccTek Laser is a professional manufacturer of laser welding equipment with over a decade of industry experience. The company specializes in helping industrial manufacturers, precision machining enterprises, and professional welding job shops successfully implement laser welding technology across a wide range of materials and applications. Its product portfolio includes: handheld fiber laser welders (1500W and 2000W) designed for flexible workshop welding and the joining of precision components; automated wire-feed laser welding systems for applications requiring filler materials and precise metallurgical control; benchtop and workstation-style laser welding systems for precision parts manufacturing; and fully integrated robotic laser welding systems equipped with six-axis articulated robotic arms, tailored for high-volume automated production.
All systems utilize high-efficiency fiber lasers from globally recognized brands—such as Raycus, JPT, and IPG—with output power ranging from 1000W to 6000W to meet diverse operational requirements. The entire product line is CE and FDA certified, ensuring compliance with global safety and performance standards.
The complete service framework includes pre-sales application assessment and process feasibility analysis for specific materials and joint configurations, professional installation and commissioning with full system integration, comprehensive operator training covering both routine operation and basic troubleshooting, parameter optimization for specific materials and production requirements, competitive spare parts supply for consumables and replacement components, and responsive after-sales technical support ensuring that laser welding systems continue operating reliably and productively throughout their service life.

Contact information
- [email protected]
- [email protected]
- +86-19963414011
- No. 3 Zone A, Lunzhen Industrial Zone,Yucheng City , Shandong Province.
Get Laser Solutions